Batch Reactors: Development, Engineering, and Construction
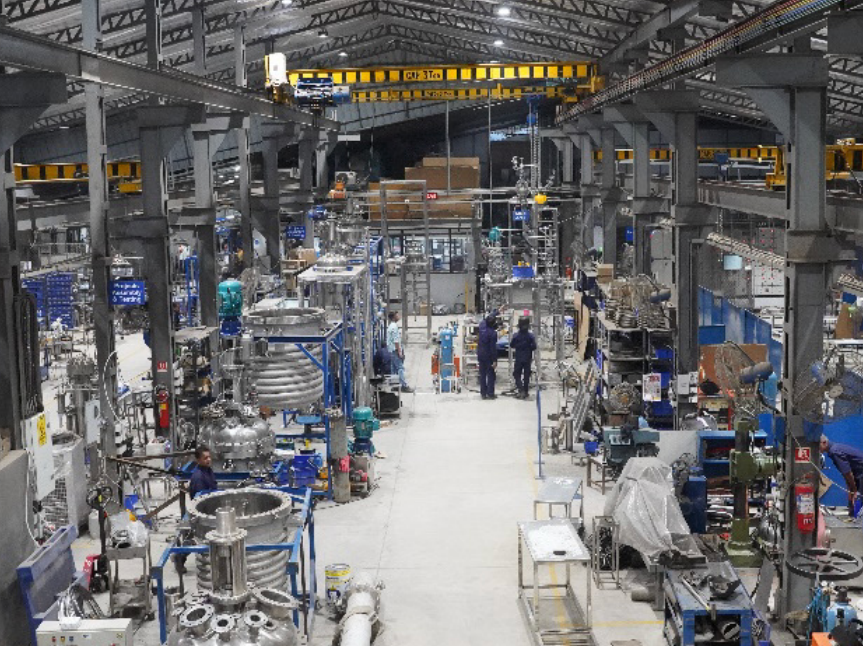
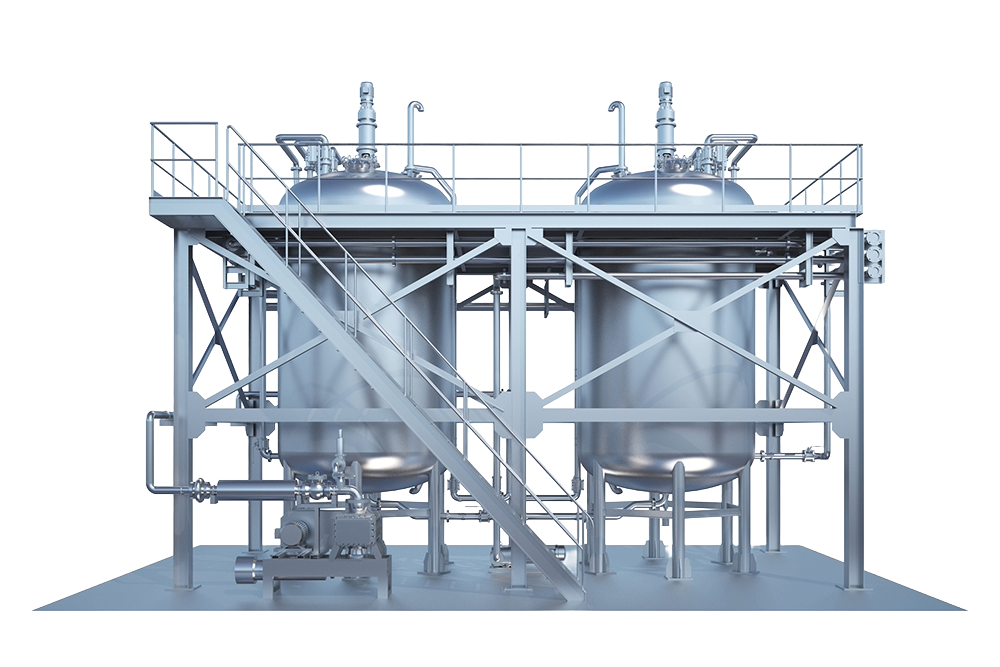
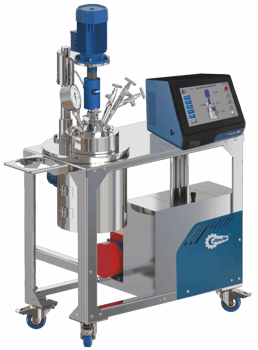
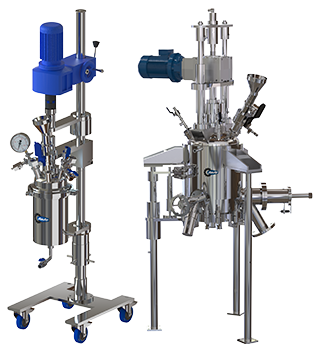
ActiveSite provides batch reactor systems for every stage of development, from lab to commercial. Our team of chemists and engineers can help you select and install new equipment or evaluate existing batch assets for retrofit.
ActiveSite is more than an equipment supplier, we are a catalyst company who understands process chemistry and the requirements for scaling and running a commercial batch operation.
ABOUT US
Why ActiveSite?
Catalyst Experts
Manufacturing catalysts for over 25 years. We combine a history of materials development with best practice chemical engineering to provide world class solutions.
Fair, Fast, Excellent
ActiveSite is part of the Applied Catalysts + Technologies group (AC+T) a family held organization that prides itself on fast delivery. Our chemists, chemical engineers, and business development teams are fast and effective and care about your success.
We Help You Scale
ActiveSite has solutions all stages of chemical development (lab to production). We offer clients experience on how to quickly commercialize technology.
What is the best way to contact ActiveSite to discuss a proprietary application?
You can reach out on our submit a quote form with a simple application description. One of our engineers will contact your and we can begin to develop you needs.
What is a typical lead time for equipment?
We offer both standard and custom batch equipment for customers. Our team recognizes the urgency of projects and will work to develop solutions that fit your timeline.
I have existing assets I would like to leverage for a new application. Can you help?
Absolutely. Our engineering and applications team can help support retrofits.
Can you evaluate chemistry in your labs?
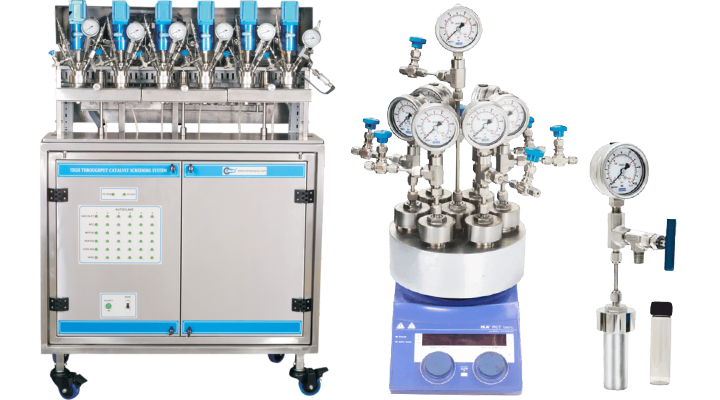
Yes, ActiveSite has high throughput multi reactors, 250 ml and 2L autoclaves for running client chemistry.
Batch Reactor Systems Overview
Batch reactor systems are available from lab scale (25 mL) to production scale (1,000 L), covering the full commercialization journey.
All systems are configurable for high-pressure (up to 350 bar) and high-temperature (up to 500°C) conditions.
Material options include SS316, Hastelloy, Inconel, Monel, Titanium, Tantalum, and glass-lined steel - selected based on process chemistry and corrosion requirements.