ActiveSite provides continuous reactor systems for every stage of development, from lab to commercial. Our team of chemists and engineers can help you select and install new equipment or evaluate existing continuous reactor assets for retrofit.
ActiveSite is more than an equipment supplier; we are a catalyst company that understands process chemistry and the requirements for scaling and running a continuous commercial operation.
ABOUT US
Why ActiveSite?
Catalyst Experts
Manufacturing catalysts for over 25 years. We combine a history of materials development with best practice chemical engineering to provide world class solutions.
Fair, Fast, Excellent
ActiveSite is part of the Applied Catalysts + Technologies group (AC+T) a family held organization that prides itself on fast delivery. Our chemists, chemical engineers, and business development teams are fast and effective and care about your success.
We Help You Scale
ActiveSite has solutions all stages of chemical development (lab to production). We offer clients experience on how to quickly commercialize technology.
My project is not in the domestic United States can you help?
ActiveSite can provide continuous reactor equipment to nearly all parts of the world.
What is a typical sized project?
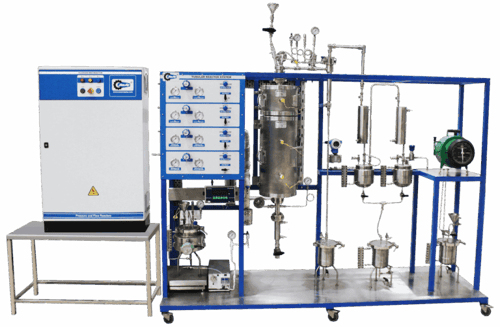
Our team can provide equipment at all scales. We offer services for full scale operation down to standard products for desktop lab development.
What areas of chemistry do you have experience?
ActiveSite has experience with a wide array of chemistry and equipment. We have executed projects for hydrogenations, hydrocarbon chemistry, partial oxidations, and more. Please see our applications area section and whitepapers for more detail.
My technology is conceptual can you help?
Yes, our team can help you. We believe great ideas often start small.
Continuous Reactor Systems Overview
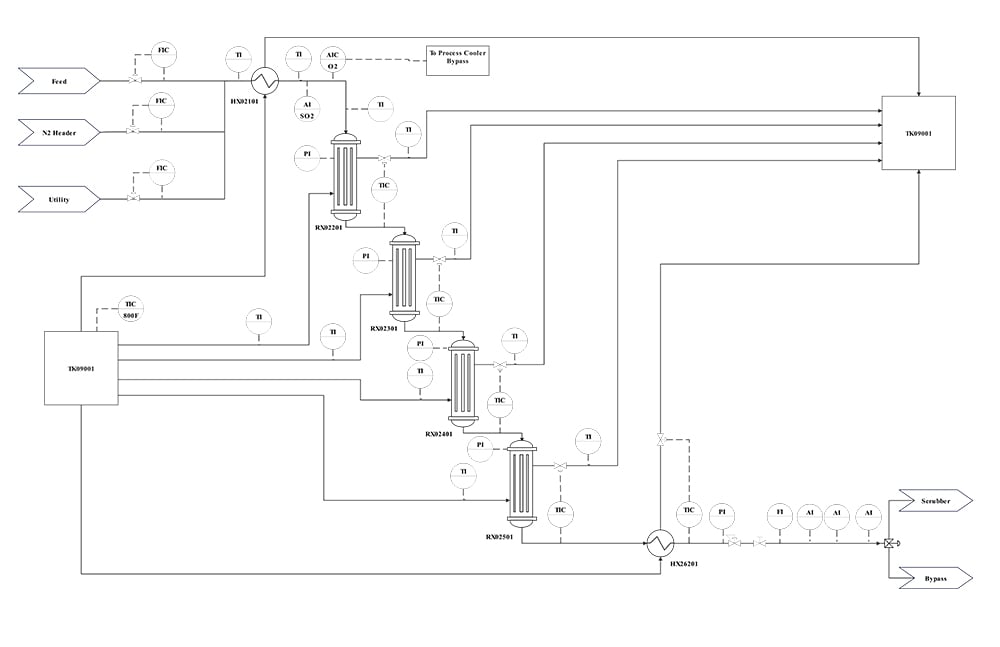
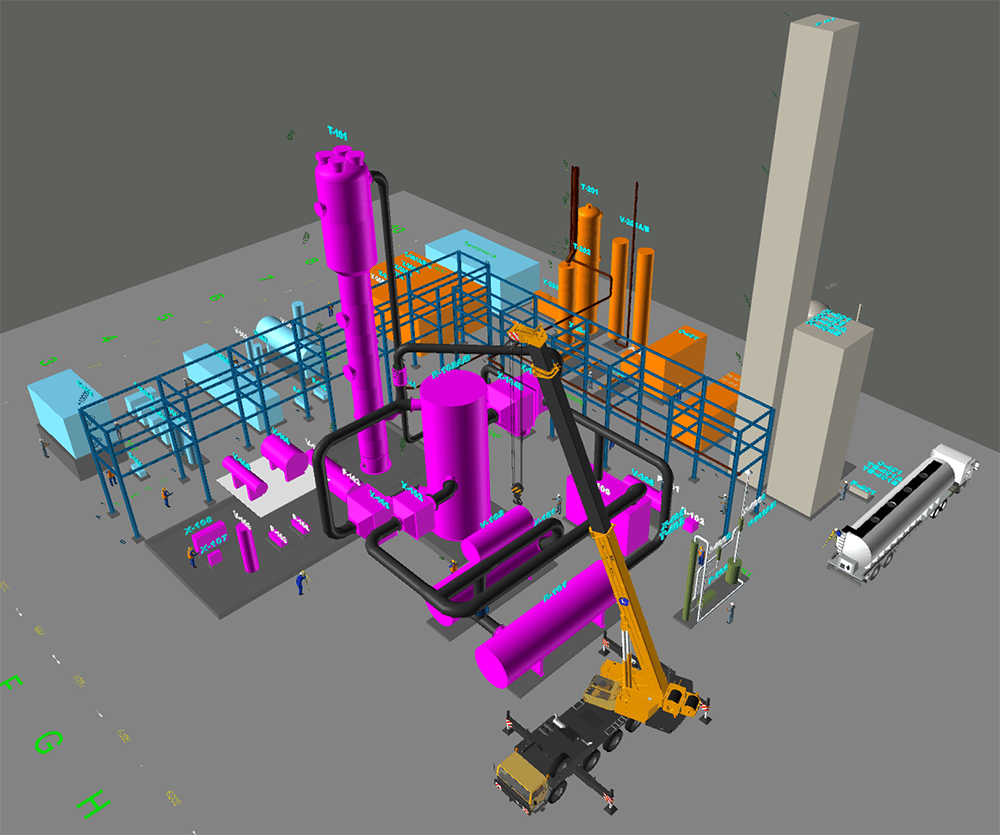
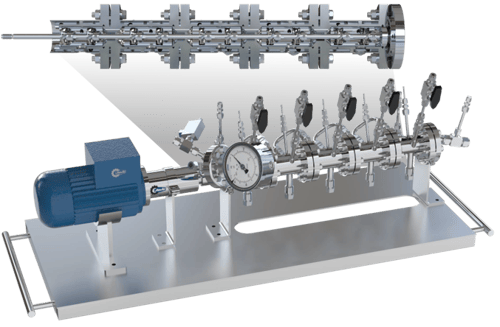
ActiveSite provides continuous reactor systems for lab, pilot, and commercial-scale applications, supporting process development from early testing through scale-up and production.
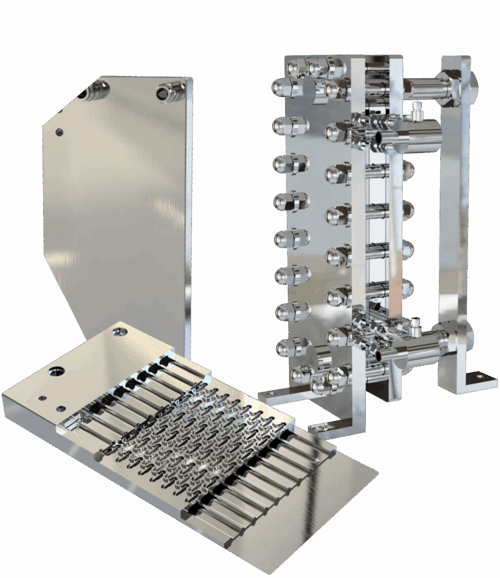
Available configurations include commercial reactor systems, custom pilot units, slurry handling reactors, and microreactors for a range of chemistry, flow, pressure, temperature, and catalyst requirements.
Systems can be configured for high-pressure and high-temperature operation, with material options selected based on process chemistry and corrosion requirements.
ActiveSite combines reactor engineering with catalyst and process expertise to help customers select, size, and scale continuous reactor systems for reliable commercial operation.
Talk to an engineer about your continuous reactor system.